Workpiece & target
Define material, allowance and acceptance criteria before choosing the abrasive or geometry.
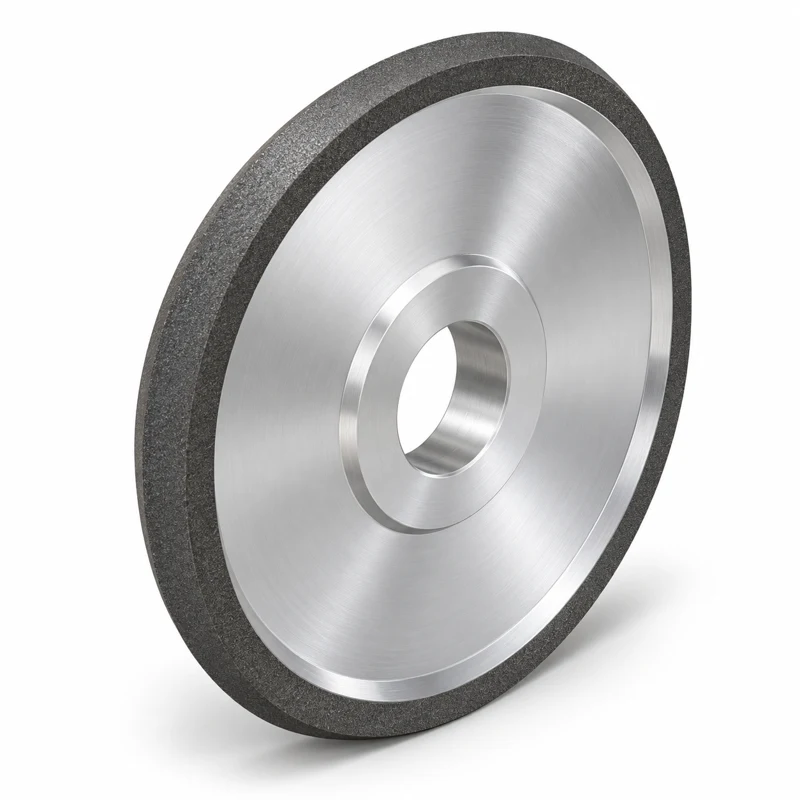
CBN profile-wheel concepts for suitable hardened ferrous gear components.
APPLICATION REFERENCE / HM-G15
Application reference, not a stock SKU. Configuration and supply require technical review.
Gear profiles; splines; application-specific hardened forms.
Develop the abrasive layer and dressing strategy around the required profile and wheel wear behavior.
Vitrified CBN gear-profile grinding requires the tooth geometry, material, form tolerance and dressing system. The active abrasive layer follows the approved profile.
Define material, allowance and acceptance criteria before choosing the abrasive or geometry.
Review mounting, access and process motion against the actual machine arrangement.
Agree the drawing and evaluation method before comparing finish, wear or process capability.
| Configuration item | Information to provide / confirm |
|---|---|
| Application-specific inputs | Alloy and hardness; gear data; form tolerance; dresser and spindle. |
| Workpiece | Material designation, hardness, heat treatment and incoming stock |
| Acceptance criteria | Drawing tolerances, form requirements, surface texture and measurement method |
| Wheel & mounting | Shape drawing; outside diameter D, width T, bore H or shank/thread connection, as applicable |
| Abrasive system | Workpiece-dependent abrasive, grain specification, bond and conditioning method |
| Machine & process | Spindle/interface, coolant, dressing arrangement and approved operating limits |
| Quantity & supply | Trial / production quantity; final configuration and availability confirmed after review |
HM-H and HM-G references identify this application collection, not inventory SKUs. Dimensions, construction, supply feasibility and lead time require confirmation.
Send a workpiece and tool drawing where available, material and hardness, machine and interface, stock allowance, finish, tolerance, coolant and quantity.
No. Images are AI-generated family illustrations. Geometry, colors and proportions are indicative; the approved drawing defines the actual tool.
Provide the actual machine model, mounting interface, spindle or feed arrangement and available clearance. A machine brand alone does not establish compatibility.
Specification and acceptance requirements are agreed for the application. Operating speed follows the approved design and actual tool marking; an illustration is not an operating instruction.
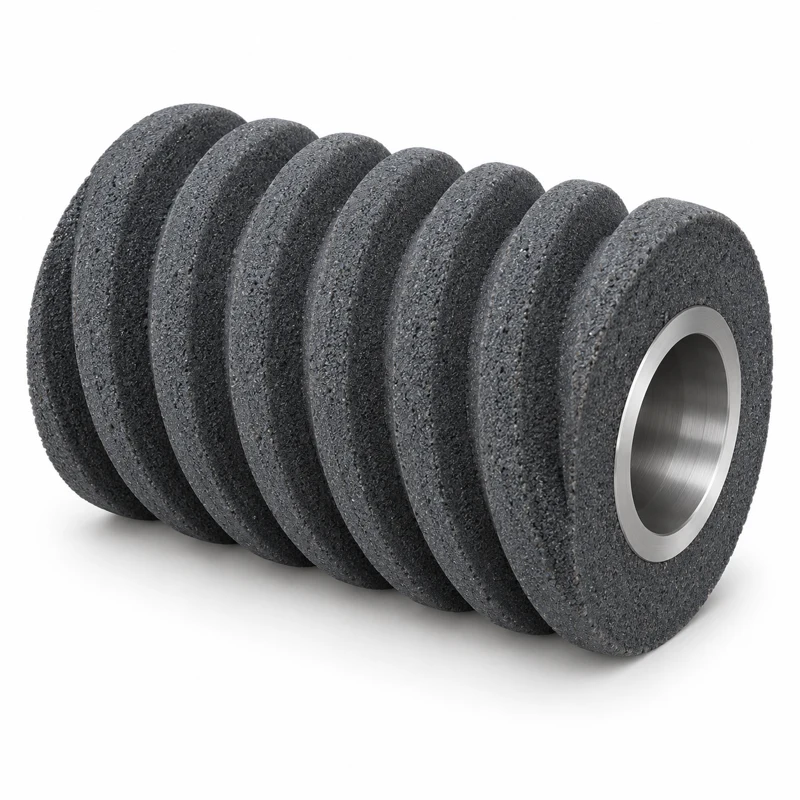
HM-G06 / GRINDING
An application pathway for continuous generating gear grinding, requiring a defined abrasive system.
View Application & Configuration →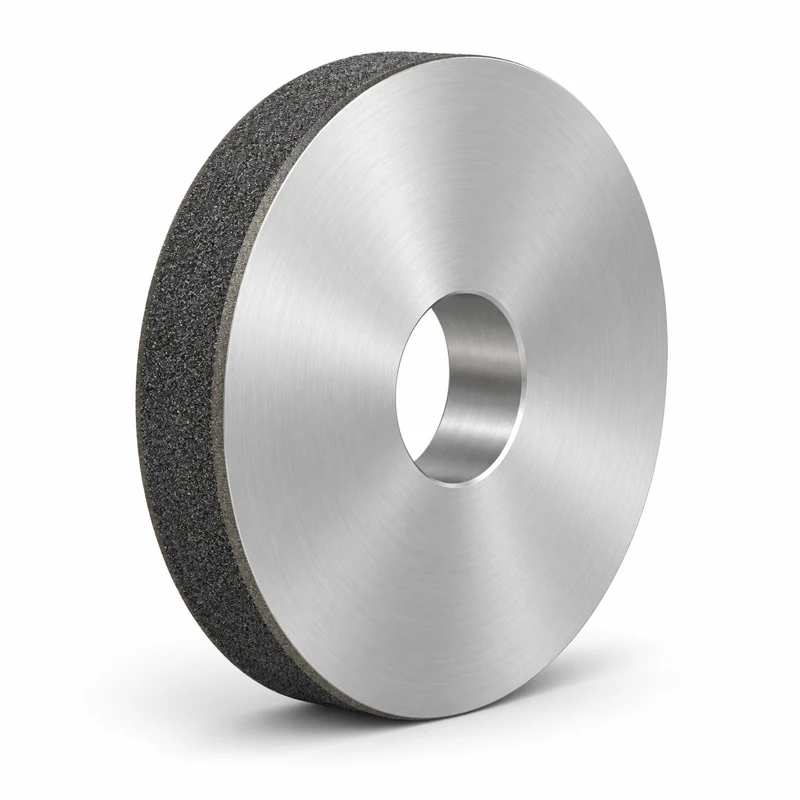
HM-G07 / GRINDING
Material-led wheel selection for external diameters, shoulders and related surfaces.
View Application & Configuration →
HM-G08 / GRINDING
A process-led route to matching small wheel forms and the workpiece material system.
View Application & Configuration →